Engineered for low-glare safety, high color rendering (CRI 90+ / CRI 95), touch/dimming capabilities, and seamlessly integrated indoor/outdoor architectural applications.
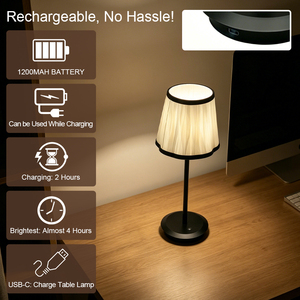
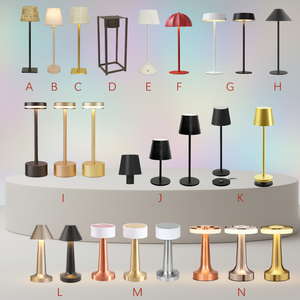
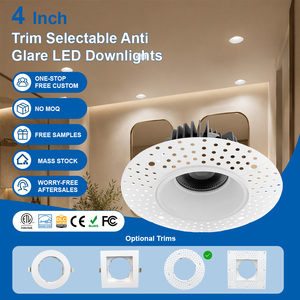
Rooted in our production facilities in Aldaia (Valencia, Spain)—traditionally operating under FM Iluminación and the Olé Lighting brand portfolio—our company stands as a premier global OEM/ODM step lights manufacturer and exporter. We bridge the gap between creative architectural design and rigorous industrial manufacturing.
Step lighting and low-level horizontal illumination require far more than basic lumen output. They demand optical precision to eliminate glare, robust thermal management within compact recessed housings, and ingress protection (IP65 to IP67) capable of withstanding severe atmospheric exposure. Our in-house research studio, metalworking workshops, and photometric testing laboratories ensure that every step light, recessed pathway luminaire, and decorative wall sconce fulfills exact specifier demands.
As architectural lighting transitions from simple illumination to human-centric, integrated spatial experiences, OEM/ODM manufacturing must evolve alongside rapid technological advancements.
Modern step lights rely on ultra-narrow asymmetric optical lenses and baffle geometries that project light strictly downward onto tread surfaces. This mitigates direct line-of-sight glare (UGR < 13) and conforms strictly to global Dark-Sky light pollution ordinances.
Architects increasingly demand trimless plaster-in step light designs. Utilizing specialized zinc-coated steel or aluminum mud-in flanges, step lights blend directly into drywall, concrete, or stone facades without visible outer borders.
Outdoor steps, poolside staircases, and coastal hospitality resorts require corrosion-resistant 316L stainless steel, fluorocarbon powder coatings, and double-O-ring silicone sealing to prevent moisture ingress and saltwater pitting over decades of operation.
The integration of Dali-2, 0-10V, and wireless Bluetooth Mesh protocols (Casambi, Tuya, Zigbee) into micro-step light drivers enables automatic dynamic color temperature shifting (2200K warm night-lighting to 4000K daylight-assisted pathing).
Integrated PIR and microwave motion sensors embedded discreetly within the step light faceplate allow step-by-step sequential illumination, drastically reducing hotel and residential corridor energy consumption by up to 78% while maximizing occupant safety.
Key structural shifts shaping how wholesalers, engineering procurement contracts (EPC), and lighting brands select OEM/ODM manufacturing partners globally.
Global distributors are shifting toward Semi-Knocked-Down (SKD) module procurement. By standardizing universal LED light engines, optical reflector inserts, and interchangeable faceplates (round, square, louvred, slotted), importers can reduce stockkeeping units (SKUs) while maintaining maximum flexibility for customized end-user requests.
Commercial tenders increasingly enforce strict embodied carbon thresholds. Procurement mandates prioritize manufacturers who utilize 100% recycled aluminum alloys, halogen-free wiring, eco-friendly powder coatings, and zero-plastic recyclable packaging. Sustainable manufacturing is no longer optional—it is a core qualification requirement.
Low-voltage step lights are moving away from harsh blue-tinted 6000K chips toward high spectrum fidelity LEDs (Color Rendering Index Ra > 95, R9 > 80, TM-30 Rf > 93). This ensures that natural timber staircases, marble steps, and tactile wall finishes retain their true organic depth and warm textures under artificial light.
Centralized remote driver systems (24V DC Class 2 power supplies) are overriding line-voltage (110V-240V AC) step lights in high-end projects. Remote drivers streamline installation, eliminate flickering inside ultra-thin wall cutouts, simplify maintenance access, and guarantee extended luminaire life spans exceeding 50,000 hours (L80B10).
Transforming concepts, CAD drawings, and strict architectural specifications into fully certified physical products.
Equipped with modern CNC machining centers, aluminum die-casting presses, and 3D rapid prototyping facilities, we can execute custom step light housing molds, custom aperture cutouts, and bespoke mounting brackets within expedited engineering timeframes.
Choose from anodized matte black, brushed brass, textured white, raw concrete, or custom RAL powder coats to match interior joinery. We engineer optical light guide plates, frosted diffusers, and honeycombed anti-glare louvers to match any beam angle specification.
We integrate high-grade LED chips (Bridgelux, Cree, Osram, Citizen) alongside premium driver modules (Tridonic, Osram, Meanwell, Lifud). Support for Mains Triac dimming, 0-10V, DALI-2, and Emergency Battery Backup modules tailored to regional voltage standards (100V–277V).
Every batch of OEM/ODM step lights undergoing production at our facilities undergoes stringent quality verification prior to export container loading:
Addressing essential technical, logistical, and customization queries for lighting specifiers, importers, and contract distributors.
Indoor step lights focus heavily on optical aesthetics, ultra-low profile trimless mounting, low visual glare (UGR), and smooth dimming integration. Outdoor OEM step lights prioritize environmental durability, featuring heavy-duty die-cast aluminum or 316 stainless steel bodies, IP65-IP67 silicon gasket seals, IK08-IK10 impact protection, UV-resistant powder coats, and built-in anti-condensation breathing valves to prevent lens fogging.
Yes. As a direct OEM/ODM manufacturer, we can engineer custom mounting plates, spring clips, or rear housing dimensions to match standard international back-boxes (such as US 2"x4" single-gang boxes, European round 60mm/68mm flush boxes, or custom masonry concrete pour-in sleeves).
Glare control is achieved through optical engineering. We incorporate deep-set recessed LED engines, 45-degree downward louvers, micro-prismatic optics, and indirect rebound reflector technology. This ensures that light rays are directed strictly downward onto the floor tread without direct diode exposure to observers ascending or descending the stairs.
For luxury hotels and high-end residential developments, warm color temperatures (2700K to 3000K) or Dim-to-Warm (3000K fading to 1800K) are standard. We recommend CRI 90 or CRI 95 with high R9 values to render natural stone, wood grain, and wall finishes vividly under low ambient light levels.
For standard catalogue modifications (custom finish colors, specific CCT, branded laser engraving), MOQs start as low as 50–100 units with a lead time of 2–3 weeks. For completely customized OEM/ODM molds, tooling development typically requires 20–30 days, followed by sample validation and mass production within 25 days.
Yes. All our products are tested and documented with CE declarations, RoHS compliance, LVD, and EMC reports. We can also configure luminaire drivers and wiring harnesses to meet specific regional requirements such as UL/ETL for North America, SAA for Australia, or SASO for the Middle East.
We incorporate onboard constant current IC regulators inside our 24V DC LED PCB modules. This allows multiple step lights to be wired in parallel along extended cable runs (up to 30 meters) without noticeable brightness attenuation or color temperature shift between the first and last fixture.
Whether you are an architect seeking custom contract manufacturing, an importer expanding your product catalog, or a lighting brand looking for reliable European-standard manufacturing in Valencia, our engineering team is ready to consult on your technical specifications.